What are the main press brake die types?
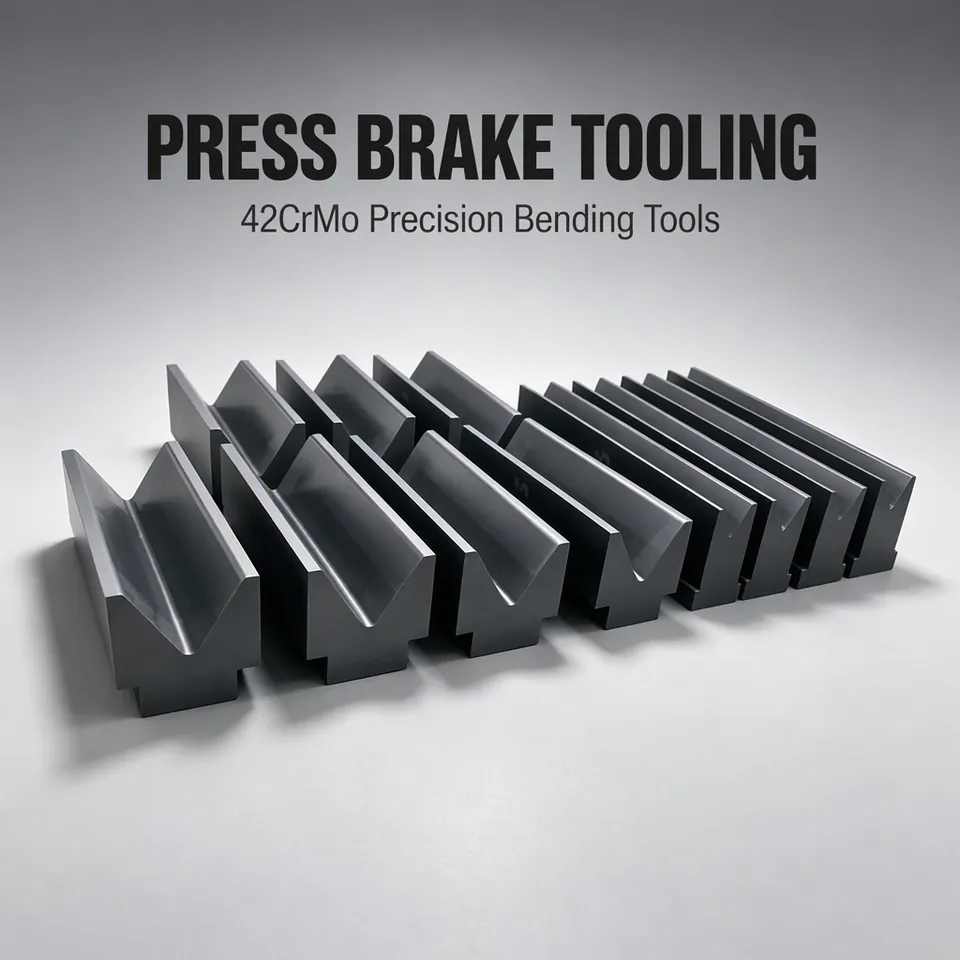
The main die types are single-V, 2V, multi-V, urethane and adjustable or roll-bending dies. Single-V is the general-purpose choice, multi-V lets one die serve several openings, and urethane produces a mar-free radius.
Die types compared
Choose the die for the opening and the finish the part needs. A single-V die is the default, and the others solve a specific problem.
| Die type | What it does | Use it when |
|---|---|---|
| Single-V | One V opening, one radius | General air bending; the standard choice |
| 2V | Two different openings in one body | Two thicknesses or radii share a machine |
| Multi-V | Several openings machined into one die | Job shop work with changing radii |
| Adjustable / roll-bending | Opening or effective angle can be changed | Variable radius, or to correct springback |
| Urethane | Elastomer insert forms the radius | Cosmetic surfaces that must not be marked |
How is a press brake die specified?
A die is specified by the V opening, the die body width and height, the shoulder radius, the overall length and the tool steel. The opening is the value that determines the bend radius and the tonnage.
- V opening: normally about eight times the material thickness for mild steel.
- Body width and height: must suit the machine's die rail or holder.
- Shoulder radius: affects marking and the achievable minimum flange.
- Length and segments: matched to the bend length and the clearance needed.
- Tool steel: chosen for wear life and the rated load.
What is the difference between a 2V and a multi-V die?
A 2V die has two openings in one body, so it serves two thicknesses or radii. A multi-V die has several openings, usually four or more, and is aimed at shops that change jobs frequently.
| Feature | 2V | Multi-V |
|---|---|---|
| Openings | Two | Four or more |
| Height | Taller than single-V | Tallest of the standard types |
| Best for | Two recurring setups | Job shops with frequent changes |
| Load per opening | Same as single-V | Same as single-V per opening |
Which die do I need for a mar-free finish?
A urethane die. The elastomer insert wraps the material around a radius instead of pressing it against steel shoulders, so the outer surface is not marked. The trade-off is a larger radius and a more limited pressure range.
Does the die opening have to be exactly eight times the thickness?
No. Eight times is a starting point for mild steel that balances radius, force and minimum flange. The opening you actually need is the one that satisfies the drawing's radius and flange, within the machine and tooling load limits.
| If the opening is | Radius | Force | Minimum flange |
|---|---|---|---|
| Narrower | Tighter | Higher | Shorter |
| Equal to 8t | Moderate | Moderate | Moderate |
| Wider | Larger | Lower | Longer |
Related technical pages
Press brake punches
Profiles that pair with each die type.
V-die opening selection chart
Opening against radius, minimum flange and tonnage.
Adjustable and multi-V dies
Dies whose effective opening or angle can be changed.
Urethane dies
Mar-free forming for coated and cosmetic sheet.
Next step
Send the material, thickness range and the radii you bend and we will recommend one die that covers most of your work.
Request a quotation